

Your Advantages
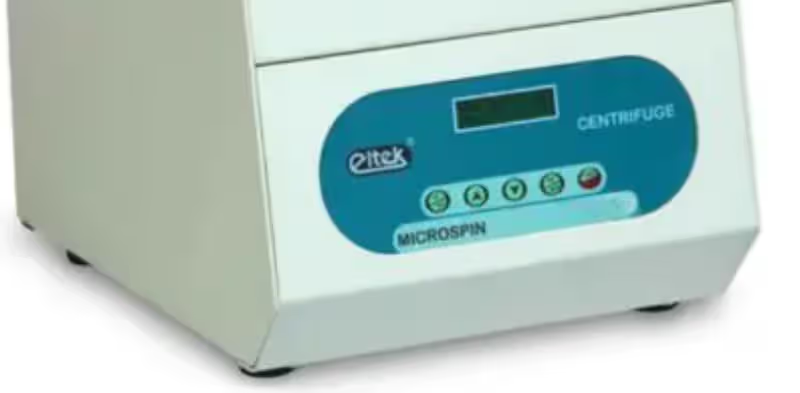
Eltek Multispin Refrigerated 300ml Centrifuge - Pack of 1 Unit (RC 650 F )
₹1,84,200
₹2,02,620
9% Off
Exclusive of 18% GST
Pack Size
Variant unavailable, Please select another variant
Similar Products
Delivery By
Enter location
Subtotal :
₹1,84,200
Want to buy bulk quantity?
Share your thoughts on this product
Incorrect Prices? Missing Information? Delivery time too high?
Brand Eltek
What's in the Box
1 Main unit
Description:The Eltek Multispin Refrigerated 300ml Centrifuge (RC 650 F) stands as a pinnacle in temperature-controlled sample processing, offering precision and versatility for laboratories engaged in advanced research and diagnostic applications. With a focus on maintaining sample integrity, this refrigerated centrifuge delivers unparalleled performance in a compact and efficient design.
Key Features:
Refrigerated Chamber Technology: The RC 650 F features an advanced refrigerated chamber, allowing precise temperature control during centrifugation. This technology is instrumental in preserving the integrity of temperature-sensitive samples, making it an ideal choice for a range of applications, from molecular biology to clinical research.
High-Capacity Processing: With a generous 300ml capacity, this refrigerated centrifuge accommodates large sample volumes. The refrigerated chamber extends its applicability to diverse sample types, providing researchers with the capability to process a variety of biological and chemical specimens.
Intuitive Touchscreen Interface: The instrument is equipped with an intuitive touchscreen interface, providing researchers with seamless control over temperature and operational parameters. This user-friendly interface enhances ease of use, allowing for efficient customization of settings for different experimental requirements.
Adaptive Speed Control: Incorporating adaptive speed control technology, the RC 650 F allows researchers to optimize rotational speeds based on specific sample characteristics. This dynamic control ensures precise separation, contributing to reliable and reproducible results in temperature-sensitive assays.
Benefits:
Preservation of Temperature-Sensitive Samples: The refrigerated chamber technology ensures precise temperature control, critical for preserving the integrity of temperature-sensitive samples. This feature is particularly advantageous in applications where maintaining sample stability is paramount.
Versatile Large-Volume Processing: The 300ml capacity, coupled with refrigeration capabilities, makes this centrifuge a versatile tool for laboratories engaged in various research and diagnostic applications.
Efficient Workflow in Controlled Environments: The intelligent touchscreen interface and adaptive speed control contribute to efficient workflow optimization in controlled temperature environments.

